Explore our high-performance certified industrial systems and precision measurement equipment.
Unmatched engineering heritage and verifiable manufacturing excellence built on rigorous compliance.
Shenzhen Mist Vape Co., Ltd. is a global Top 3 high-end vape hardware manufacturer focused on CBD/THC, with years of deep expertise in product and technology fields. Since its establishment, ASMVAPE has served hundreds of cannabis manufacturing companies in the United States, Canada, and other regions, providing excellent equipment and services.
Over the past 5 years since its founding, the company has secured over 200 globally authorized and pending patent technologies, with cumulative sales exceeding $90 million USD. The workforce has grown from an initial 120 employees to over 800, making it a medium-sized company capable of massive tier-1 global deployment.
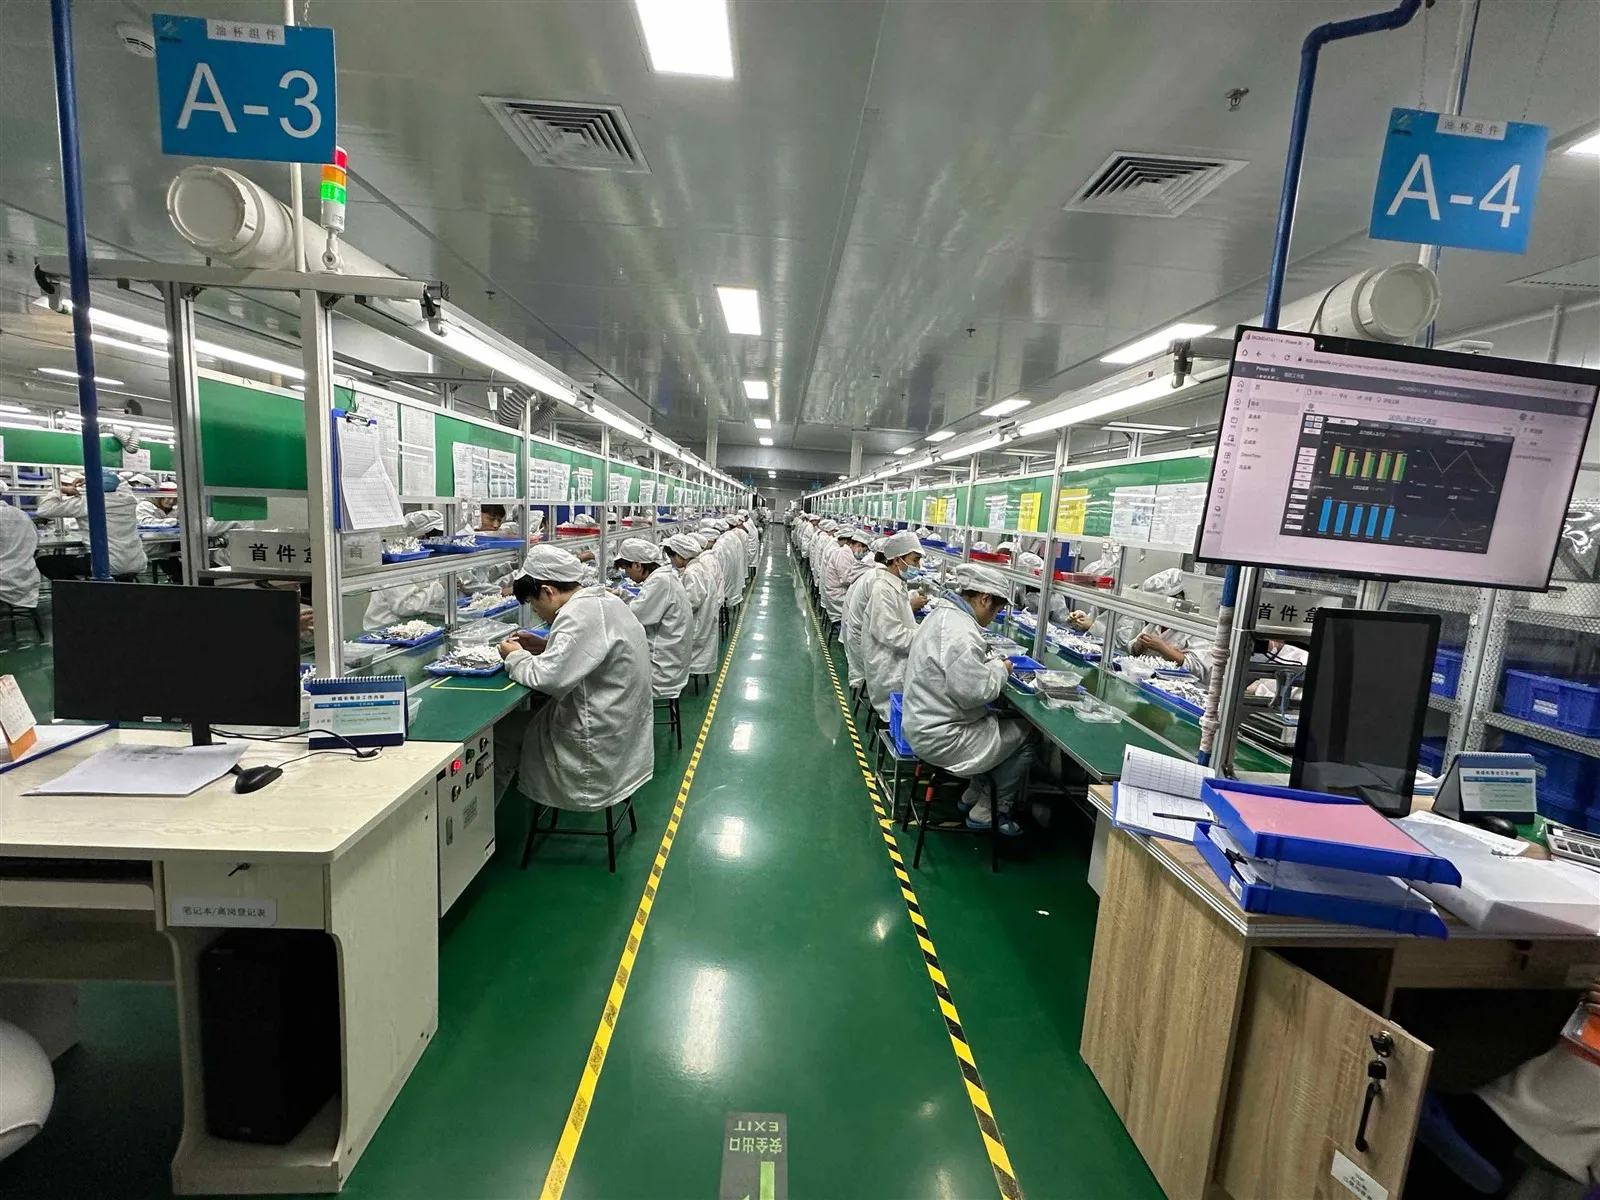
Industry-leading technical talent delivering precision product architecture and localized on-site support.
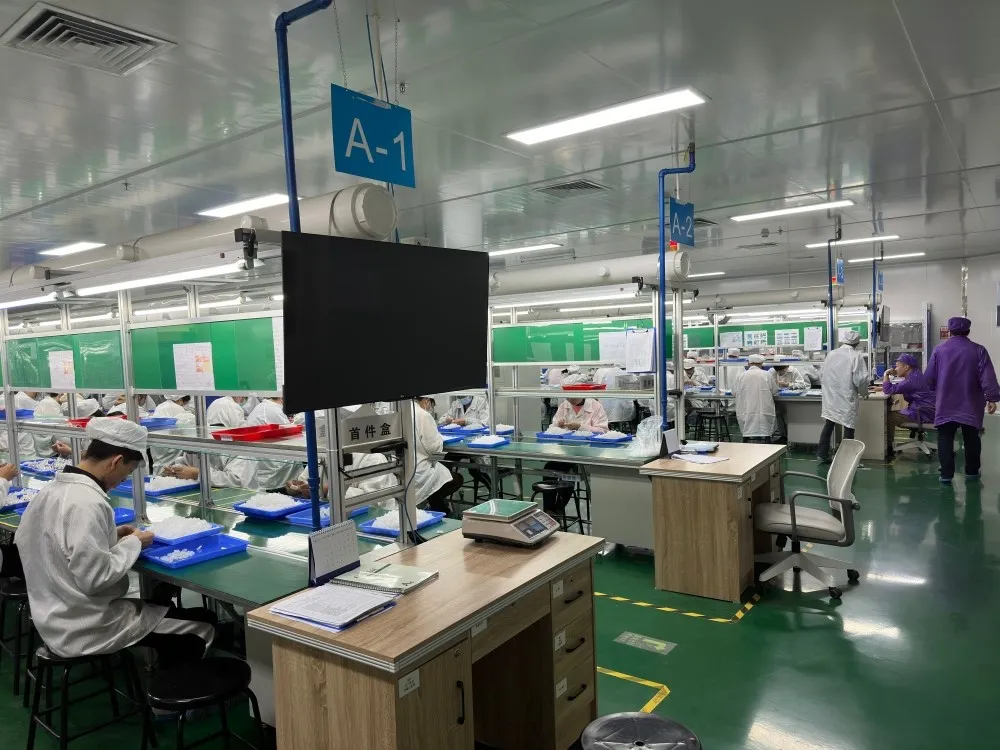
Our R&D team, partially composed of professionals from well-known industry companies such as SMOOER, ALD, and BBTANK, currently consists of more than 60 researchers involved in client projects, product development, testing, and more.
Meanwhile, to better support our global clients, we operate a large product laboratory in California, where our engineers can be dispatched to customer sites at any time for hands-on technical guidance.
Shenzhen Mist Vape Co., Ltd. adheres to the core philosophy of quality optimization, prioritizing product quality and health services to meet customers' demands for high-quality atomizers and cutting-edge adjustable airflow systems.
Pioneering next-generation atomization through intelligent thermodynamics and material science innovation.
Integrating micro-sensor chips to auto-calibrate resistance and airflow delivery, ensuring consistent vapor density across varying viscosity profiles in CBD and THC extracts.
Developing porous nano-ceramic heating elements designed to eliminate heavy metal leaching while providing rapid thermal ramp-up times under 0.05 seconds.
Transitioning toward biodegradable chassis polymers and recyclable medical-grade stainless steel assemblies to meet strict international environmental mandates.
Navigating complex global regulatory landscapes with turnkey compliance and localized OEM/ODM solutions.
Our manufacturing protocols fully align with ISO9001, GMP, and PMTA-ready standards. Every batch undergoes rigorous heavy metal, emission, and chemical stability testing to guarantee absolute safety for North American and European markets.
From initial concept sketching and 3D fluid-dynamics simulation to mass industrial production, our comprehensive engineering ecosystem provides B2B brand partners with end-to-end proprietary product development.
Discover additional specialized automation devices, precision testing tools, and commercial appliances.
Expert insights addressing critical procurement and technical inquiries for global B2B buyers.
With over 200 authorized patents, a dedicated R&D team comprising alumni from industry giants like SMOOER, ALD, and BBTANK, and rigorous ISO-certified production lines, we provide unmatched precision, leak-proof engineering, and custom airflow tuning for high-end extracts.
Our California-based product laboratory enables rapid prototyping, direct engineering consultations, and immediate on-site technical support, drastically reducing communication friction and time-to-market for North American brands.
As a medium-to-large scale manufacturer with over 800 skilled employees and robust supply chain resilience, we offer scalable production tiers tailored to both emerging brand startups and established global enterprises.
Every atomization device undergoes strict chemical testing, heavy metal screening, and electrical safety validation in our advanced internal laboratory, complying fully with international regulatory requirements including CE, RoHS, and FDA guidelines.
 Mist Vape